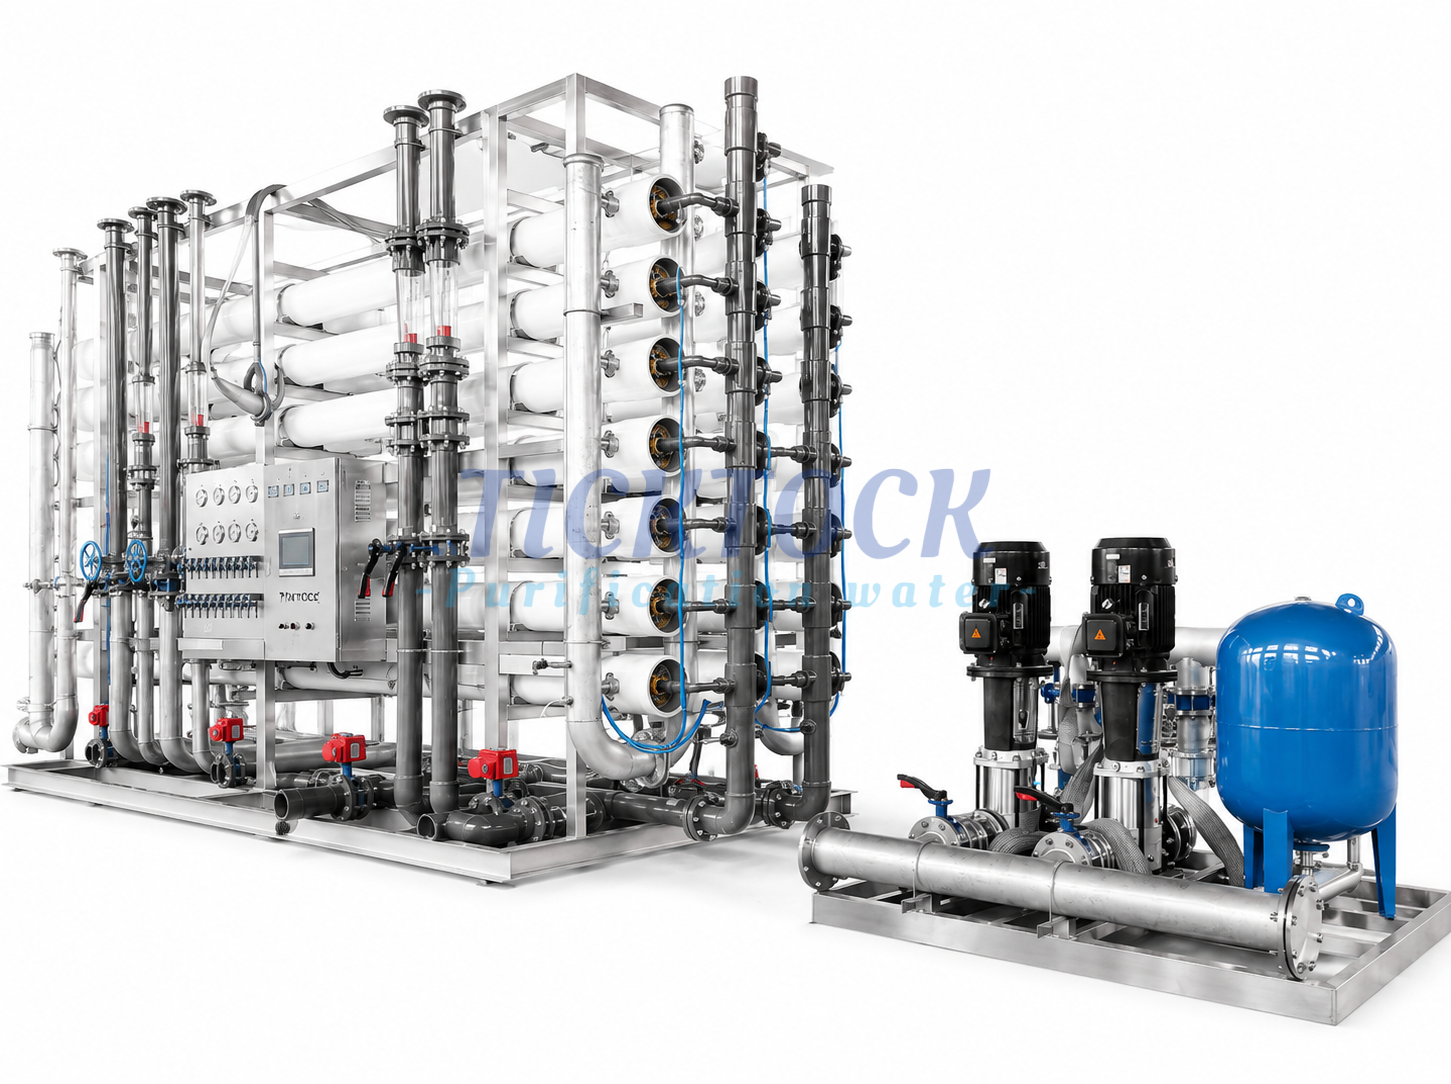
This 50m³/h RO water treatment plant is a turnkey solution customized for a mining enterprise in Mozambique. The raw water is local mine groundwater, which contains high turbidity, dissolved salts and trace heavy metals. The client needs stable process water for ore washing and production. Our solution adopts full pretreatment + single-stage reverse osmosis process. The system runs automatically, adapts to unstable raw water quality in remote mining areas of Mozambique, and greatly reduces the cost of water consumption for the mine.
Core Advantages
- Customized design adapted to Mozambique mine raw water characteristics, strong anti-pollution ability of RO membrane elements
- Fully automatic operation, less on-site manual operation, fit the remote mining site condition
- Modular structure, convenient for container transportation and field installation
- Complete online monitoring: pressure, flow, conductivity, with overload and low pressure protection
- Simple spare parts, easy for local maintenance and after-sales support
Process Flow
Raw Water Tank → Raw Water Pump → Multi-media Filter → Activated Carbon Filter → Softener → Security Filter → RO High Pressure Pump → RO Membrane System → Produced Water Tank
Scope of Supply
All filters, high pressure pump, RO membrane housings, reverse osmosis membrane elements, instrument sensors, PLC control cabinet, piping, valves, on-site installation guide, operation manual and training.
FAQ
Q1: Why is single-stage RO selected for this Mozambique mining project instead of double-stage RO? A1: The client’s production water requirement does not need ultra-pure water. Single-stage RO can meet the water standard and control the project investment and operation cost better.
Q2: Can this system adapt to unstable power supply in Mozambique mining area? A2: Yes. We configure low voltage protection, delay restart function to avoid membrane damage caused by frequent power fluctuation.
Q3: What after-sales service can you provide for the project in Mozambique? A3: We provide drawing documents, remote online debugging guidance, operation training and spare parts supply. We can also arrange overseas technical service if needed.
Q4: How about the anti-fouling performance for mine water? A4: The pretreatment section is strengthened, equipped with automatic backwashing and chemical cleaning (CIP) system to reduce membrane fouling.